Sequential Following
The tool enters a blind hole previously threaded by a taper or plug tap.
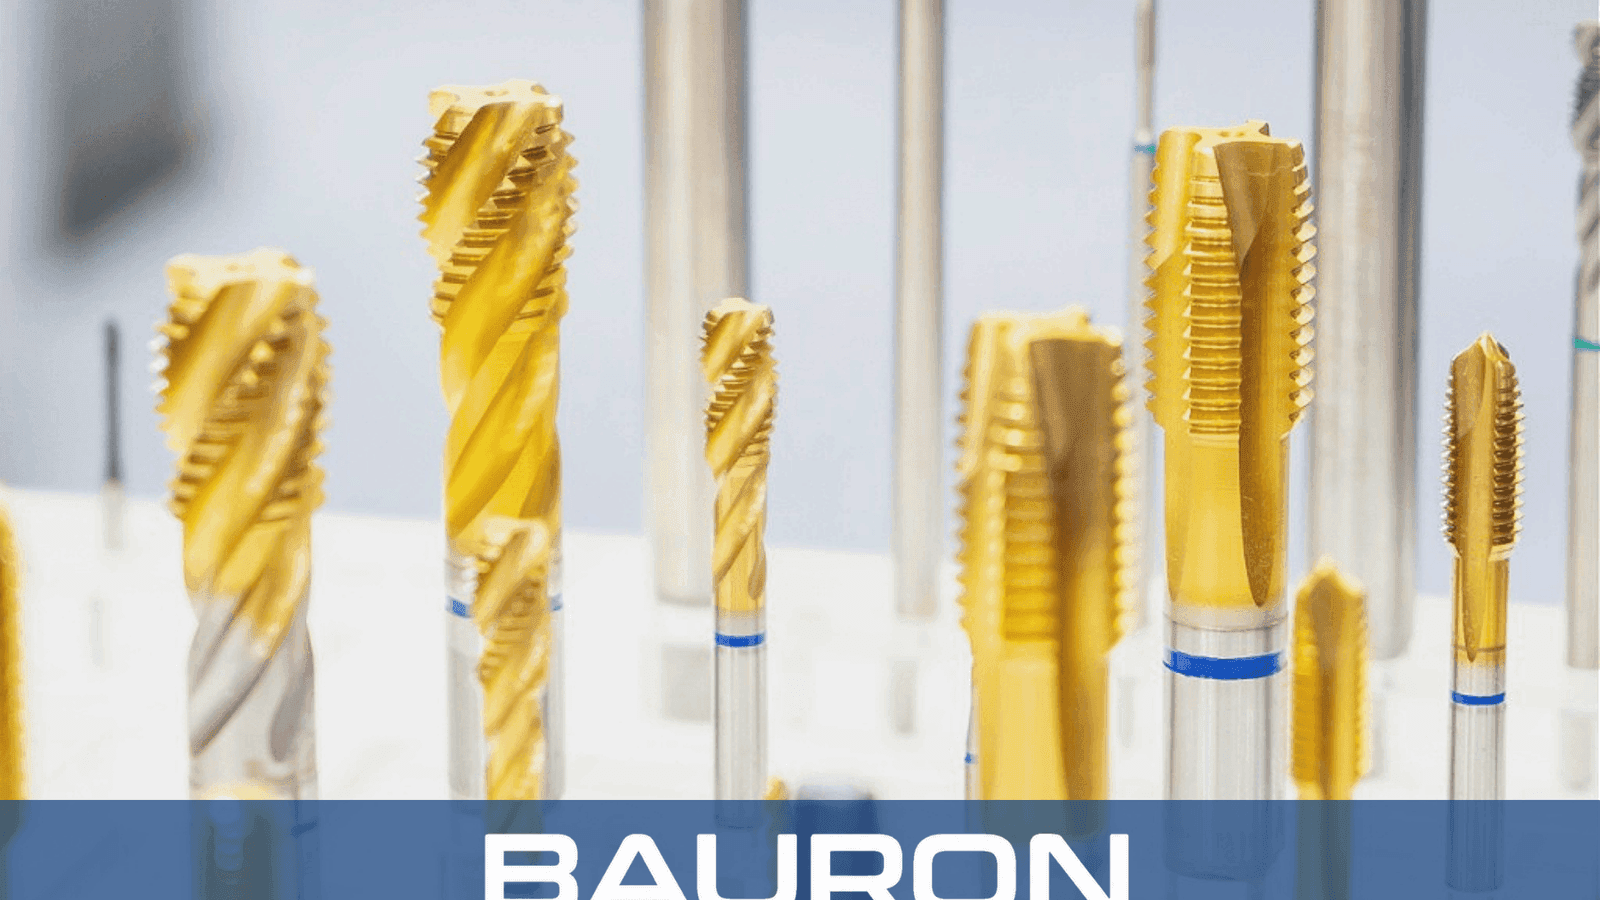
Bottoming taps are finishing tools for internal threads. Their short lead chamfer, typically 1 to 2 threads, follows a thread started by a taper or plug tap and extends the full thread profile closer to the floor of a blind cavity.
The tool enters a blind hole previously threaded by a taper or plug tap.
The short lead engages the remaining unthreaded material near the base of the cavity.
Full-size teeth behind the chamfer form thread crests and roots close to the available hole depth.
The selected flute geometry provides space to manage the remaining chips in the blind cavity.
The short lead leaves less incomplete thread near the blind-hole floor than plug or taper taps.
One to two chamfered threads permit cutting close to the available cavity depth.
Ground cutting geometry supports clean internal threads when matched to the required fit and process.
The core supports torsional stiffness, but depth control remains necessary to avoid contact with the hole floor.
Bottoming taps can be paired with matching taper and plug taps in a complete manual threading sequence.
| Specification | Range / Details |
|---|---|
| Diameter Range | #0 to 2"+; metric M1.6 to M50+ available |
| Chamfer Profile | 1 to 2 tapered lead threads; bottoming lead |
| Thread Forms | UNC, UNF, metric, NPT, and specialty threads |
| Flute Geometry | Straight flute, spiral flute, or modified bottoming geometry |
| Shank Type | Standard square drive or straight cylindrical |
| Tolerance | GH and H-class precision options |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS (High-Speed Steel) | Mild steel, brass, and aluminum. | Toughness helps resist chipping under the higher torque of a short lead. |
| Cobalt (HSS-Co) | Stainless steel, titanium, and hard alloys. | Improved hot hardness supports edge retention under friction and elevated temperatures. |
| TiAlN / TiCN Coating | Higher-volume industrial production. | Lower friction can help reduce galling in confined blind-hole cutting. |
HSS provides toughness for general materials, cobalt improves hot hardness in demanding alloys, and TiAlN or TiCN coatings can reduce friction and galling in production use.
Use rigid tapping cycles and controlled depth to finish blind-hole threads.
Hold the tap in a turret or tailstock arrangement for axial blind-hole threading.
Provide the final hand-controlled pass in a traditional multi-tap sequence.
Extends usable internal threads close to the floor of non-through cavities.
Finishes blind bolt holes and internal passages where controlled thread depth is required.
Prepares blind internal ports that require substantial fastener thread engagement.
Follows the tap drill and starting tap in a controlled blind-hole process.
It is generally unsuitable because the 1-to-2-thread lead concentrates the starting load and provides limited guidance. Start with a taper or plug tap unless the tool and process are specifically engineered otherwise.
A typical sequence uses a correctly sized tap drill, a taper or plug tap to establish the thread, and a bottoming tap to extend full-form threads closer to the cavity floor.
Use accurate hole-depth and tapping-depth control, provide chip space, apply suitable cutting fluid, clear chips as needed, and do not force the tap against the hole floor.
Spiral flutes pull chips toward the hole entrance and are commonly selected for blind holes in long-chipping materials. Straight flutes retain chips in their valleys and may require more frequent clearing.
Application-specific designs can include custom pitches, lead chamfers, flute geometry, shank dimensions, coolant delivery, and coatings.
Bauron provides design and engineering support for custom thread geometries, lead chamfers, flute forms, shank configurations, and application-specific coatings. Share the blind-hole depth, workpiece material, and process conditions for technical review.
Talk to Engineering