Initial Drilling
The front section acts as a drill and creates the rough hole diameter.
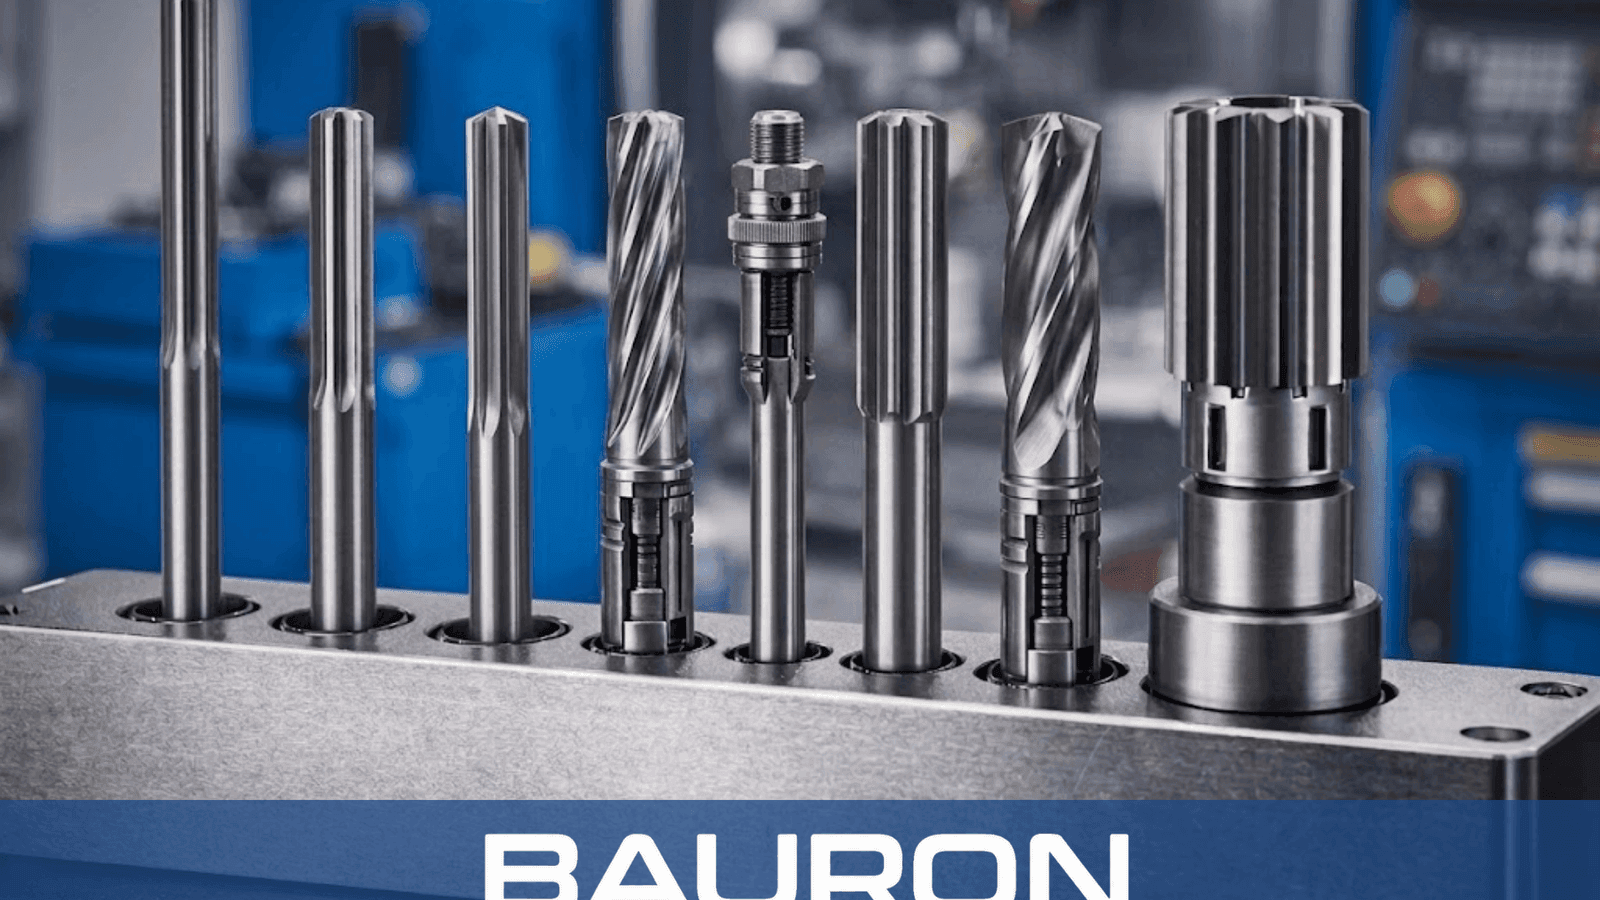
A combination reamer merges drilling and reaming into one cutting tool. This drill-reamer architecture creates the initial hole and then finishes it without a tool change or separate indexing step.
The front section acts as a drill and creates the rough hole diameter.
The following fluted section sizes the newly drilled hole to its final dimension.
Both cutting sections share an axis, which reduces the alignment variation that can occur between separate drilling and reaming setups.
Combines drilling and reaming to reduce cycle time.
Limits alignment differences between the drilling and finishing sections.
Reduces machine idle time between drilling and reaming.
Supports chip evacuation from both cutting zones.
Can incorporate stepped diameters, tapers, or application-specific bore profiles.
Is designed to resist deflection under the combined drilling and reaming forces.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/8" to 1-1/2", with custom diameters available |
| Drill Section Type | Twist or point-ground geometry |
| Reaming Section | Straight, spiral, or step profiles |
| Shank Type | Straight, Morse taper, or Weldon |
| Tolerance | Precision ground to OEM or customer specifications |
| Number of Flutes | Variable according to tool diameter |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Solid Carbide | High-speed, high-volume production. | Provides hardness and wear resistance for continuous cycles. |
| Cobalt Steel (HSS-Co) | General-purpose use and interrupted cuts. | Provides toughness and heat resistance during drilling. |
| Titanium Aluminum Nitride (TiAlN) | Dry machining and demanding cutting conditions. | Can reduce friction and material buildup on the cutting edges. |
Solid carbide provides wear resistance for stable high-volume production, cobalt steel adds toughness for general and interrupted cutting, and TiAlN can reduce friction and material buildup.
Run automated drilling and reaming in a single tool cycle.
Use combination tools to reduce cycle time in high-volume production.
Finish holes in rotating cylindrical workpieces through automated cycles.
Drills and finishes mounting holes in engine components in one cycle.
Creates and finishes holes for close-fitting aerospace fasteners.
Combines two cutting steps to reduce cycle time and increase automated-line throughput.
Supports production where cycle speed and hole-to-hole consistency are key process requirements.
Combining both operations reduces cycle time and keeps the drilling and finishing sections on the same axis without a tool change.
Application-specific tools can be designed for materials ranging from mild steel and aluminum to hardened stainless steel and aerospace alloys by selecting the appropriate substrate and coating.
The drilling and reaming sections experience different wear patterns, so tool life can differ from dedicated single-purpose tools. The cycle-time benefit must be weighed against that wear behavior.
Machine rigidity, a precision tool holder, and coolant flow that clears chips from both cutting zones affect the resulting alignment and size.
A custom tool can combine multiple stepped diameters, tapered features, or specialized chamfers in one cutting sequence.
Bauron provides design and engineering support for custom combination-tool diameters, step or taper profiles, shanks, flute geometries, substrates, and coatings. Share the complete hole print and cycle requirements for technical review.
Talk to Engineering